Bonded fabric is a composite material made by joining two or more layers so they function as one material in use. The layers might be fabric-to-fabric, fabric-to-foam, fabric-to-film or another specified combination. The joining system may use an adhesive, heat and pressure, ultrasonic energy or a process designed for a particular substrate.
That definition is intentionally broad. “Bonded” tells you that layers have been joined; it does not tell you the fiber content, exact construction, number of layers or finished performance. One bonded fabric may be a soft knit joined to fleece. Another may pair a woven face with a film. A third may combine textile and foam for a non-apparel application.
Bonding can change bulk, stiffness, drape, stretch, breathability, surface feel and sewing behaviour, but the direction and size of each change depend on the actual components and process. It does not automatically make a fabric warm, waterproof, windproof, breathable or durable.
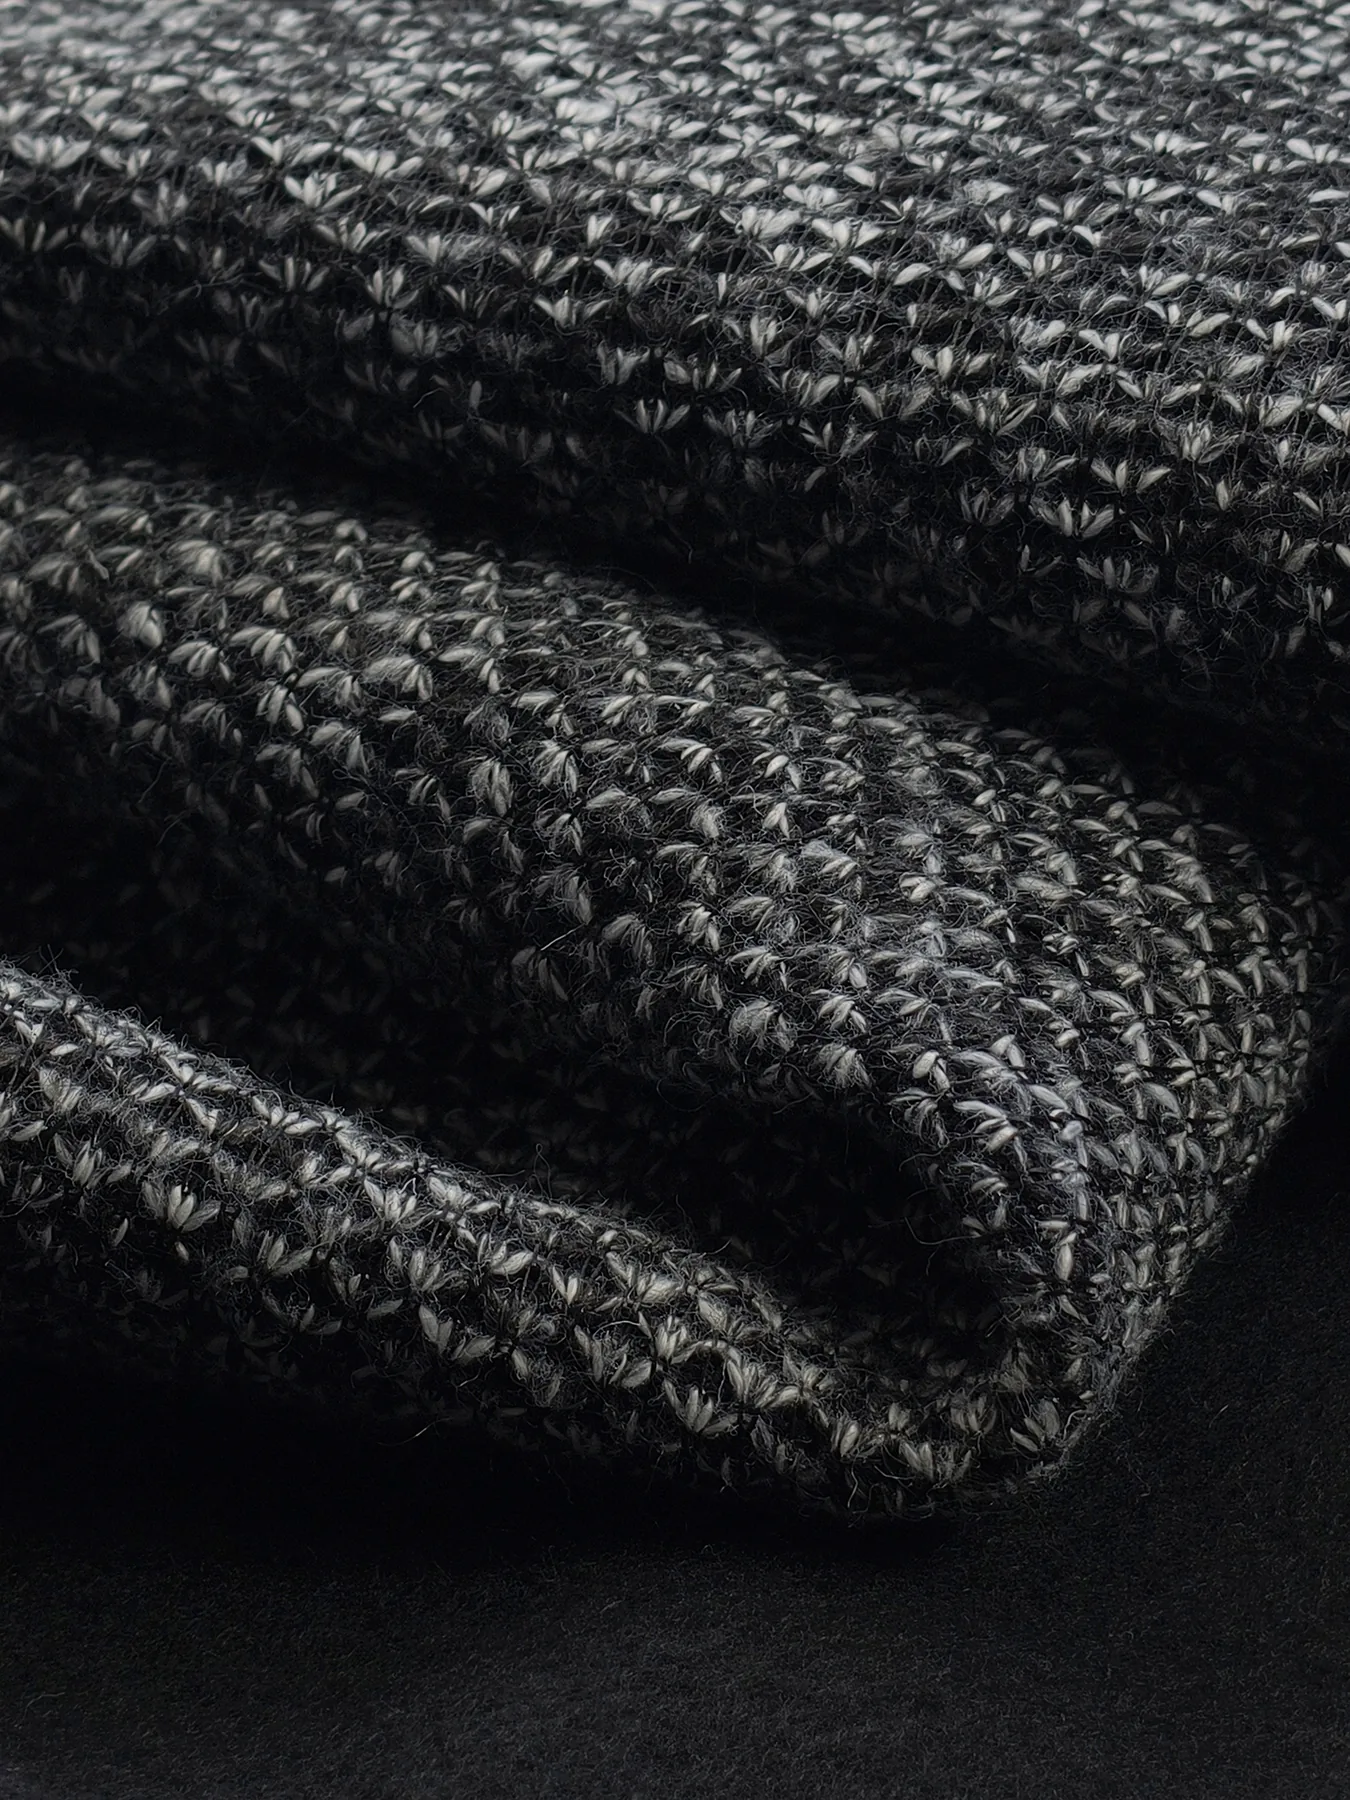
Quick answer
A bonded fabric normally has:
- at least two joined material layers;
- a face layer selected for appearance or outside performance;
- a backing, film, foam or second textile selected for another function;
- an adhesive or another joining mechanism between or at parts of the layers;
- combined behaviour that can differ from either component used alone.
To evaluate one, identify every layer, ask how the layers were joined, inspect the cut edge and both surfaces, measure stretch in each direction, sew the intended construction and test bond strength before and after the relevant care or exposure cycle.
What does “bonded fabric” mean?
In everyday textile sourcing, the term usually describes separate materials that have been joined into one composite. ANDRITZ defines lamination as combining at least two different materials to create a new composite. That is a useful engineering starting point because it focuses on the assembled stack rather than on one surface alone.
The individual layers may still be recognizable at a cut edge. For example, a face knit and a fleece backing can keep their own loop or pile structures even though they are joined. In other constructions, a very thin adhesive web or film may be difficult to see without magnification. A visual inspection can reveal likely layers, but it cannot identify the adhesive chemistry or prove bond strength.
“Bonded fabric” is therefore not a fiber name. A supplier may bond polyester to polyester, nylon to a membrane, fabric to foam or another compatible combination. Composition must come from the technical record or an appropriate analysis. For US consumer textile labeling, the FTC Textile Fiber Rule requires covered products to disclose constituent fibers using their generic names and percentages. The word “bonded” cannot replace that information.
How are fabric layers bonded together?
There is no single bonded-fabric process. The converter selects a joining route around the substrates, end use, handfeel, production speed and required resistance to care or environmental exposure.
Adhesive lamination
An adhesive is applied between the materials, the layers are brought together, and the system is set or cured under controlled conditions. Bostik's technical brochure describes powder, web, film, ordinary hot-melt, reactive hot-melt and liquid adhesive options. Covestro separately describes adhesive lamination using thermoplastic or moisture-curing polyurethane hot melts, followed by adhesion, cooldown and curing.
The adhesive can be applied as a continuous film, web, powder, dots or another controlled pattern. Coverage matters: a continuous layer and a spaced dot pattern need not produce the same hand or air pathway. Bostik notes that dot application can support breathability and softer haptics in specific systems, but that is a design option—not proof that every dot-bonded fabric is breathable or soft.
Thermal lamination
Thermoplastic components can be activated with heat and pressure. ANDRITZ describes a thermo-laminating calender in which at least two layers are bonded between rolls using pressure and temperature. Covestro describes hot-melt lamination of films with woven, nonwoven and knitted substrates.
The temperature, pressure, dwell time or line speed, and cooling conditions depend on the materials and adhesive system. Bostik's technical brochure treats pressure, time and temperature as matched process variables. Qualify the production recipe for the actual stack rather than copying settings from another fabric.
Ultrasonic bonding
Ultrasonic equipment uses high-frequency vibration to generate localized heat at contact points. In the ANDRITZ system, thermoplastic fibers melt and weld at engraved points while surrounding material receives less heat. This route is especially associated with compatible thermoplastic materials and engineered patterns. Its presence cannot be inferred from a normal product photograph.
Flame lamination
Flame lamination is a distinct, substrate-specific process. Covestro describes passing polyurethane foam over an open flame to create a thin molten surface that bonds to another layer. Because this description is foam-specific, “flame laminated” should never be used as a generic synonym for all bonded textiles.
When asking how a material was made, request the actual process family and layer stack. “Laminated” or “bonded” alone is not enough to reproduce a quality.
Bonded, laminated, coated and fused: are they the same?
The terms overlap in commercial language, but they should not be treated as perfect synonyms.
| Term | Practical meaning | What still needs verification |
|---|---|---|
| Bonded | two or more materials are joined to act as one composite | layer identities, joining route, coverage and bond requirement |
| Laminated | a common industry term for building a multilayer composite | whether the middle layer is adhesive, film, foam or another material |
| Coated | a coating material is deposited or formed on a substrate surface | coating chemistry, side, add-on, continuity and intended function |
| Fused | often used for heat-activated joining, such as an interlining bonded to another fabric | activation conditions, bond area and care durability |
A laminated textile may include a membrane or film, but a bonded fabric does not automatically contain one. A coated fabric may have a polymer layer on a textile without being a fabric-to-fabric laminate. The purchase specification should describe the actual cross-section instead of relying on one category word.
What are the layers in a bonded fabric?
The simplest way to understand a bonded fabric is to read it as a stack.
Face layer
The face is the surface intended to be seen or exposed in the finished product. It may contribute colour, texture, abrasion behaviour, printability or appearance. It can be woven, knitted or nonwoven.
Joining layer or joining points
The middle may be a liquid adhesive after curing, a hot-melt web, powder, film or localized weld points. It may cover the full area or only selected points. It is often visually subtle, yet it can strongly influence stiffness, drape, air flow and peel behaviour.
Backing or functional layer
The backing may be another textile, pile, foam, film or reinforcement. It can change the feel against the body, add thickness, stabilize a face material or contribute a specific barrier or cushioning function. Those outcomes belong to the exact backing and construction; the mere presence of a backing proves none of them.
A three-layer laminate may place a film between two textiles. A two-layer bonded knit may have no membrane at all. Ask for a layer-by-layer description, including each layer's construction and fiber content, rather than accepting a single overall description such as “polyester bonded fabric.”
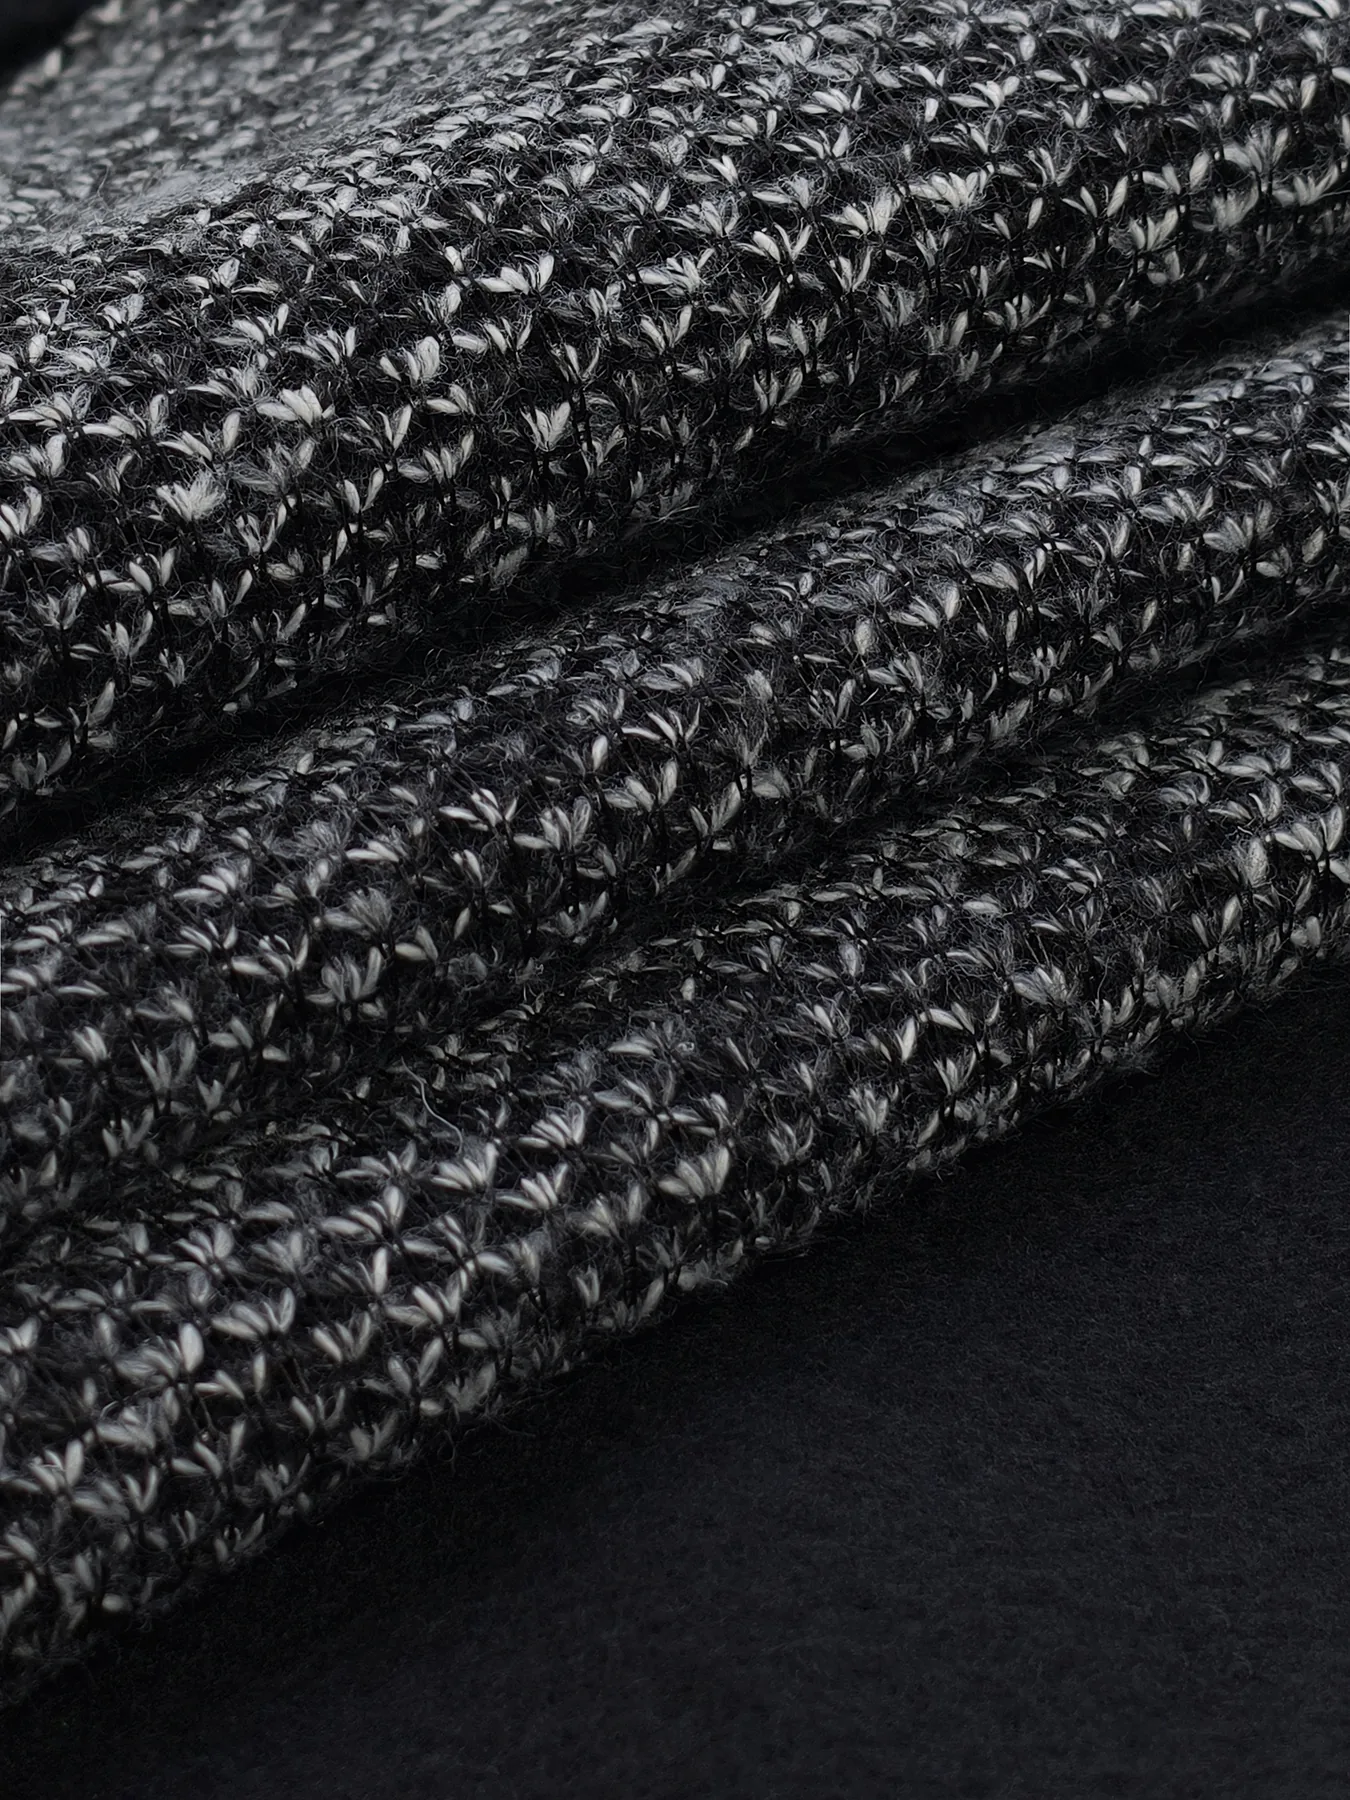
How can bonding change warmth, stiffness and drape?
Bonding changes the material because the layers must bend, stretch and recover together.
Warmth and bulk
Joining a raised, pile or foam backing to a face changes the thickness and bulk of the complete material. That may support a warmer design, but warmth is not created by the word “bonded.” A thin fabric-to-film laminate can remain comparatively low bulk, while a fabric-to-fleece composite can be much thicker. Thermal performance should be evaluated on the finished stack under an agreed method if the claim matters.
Stiffness and drape
Two flexible layers can produce a less flexible composite because the joining layer restricts movement between them. Adhesive chemistry, add-on, coverage pattern, component thickness and direction all matter. A full film may behave differently from a discontinuous web or dot pattern. The result may feel firmer, boardier, more supported or simply heavier—but those are sample observations, not universal bonded-fabric properties.
To compare drape, condition the samples consistently, cut them in the same direction and compare the complete bonded material with its individual components where available. Record the result rather than relying only on “soft” or “good drape.”
Stretch and recovery
The composite normally cannot be understood by testing only its most elastic layer. A stable backing or relatively rigid adhesive film may limit the extension of a stretchy face. An elastic adhesive or engineered pattern may preserve more movement, but it does not guarantee the original stretch.
Measure the finished composite lengthwise and crosswise. ISO 20932-1 describes strip or loop methods for elasticity and related properties. A defensible result states the direction, conditioning, load or extension cycle, number of cycles and residual growth or recovery. Never reuse the stretch percentage from one component as the value of the bonded fabric.
Air and moisture pathways
Air permeability and water-vapour behaviour depend on the whole stack. A continuous film can block pathways that were open in the face textile. A porous web or dot pattern may leave more open area, while a purpose-designed membrane may manage water and vapour in a specific way. These are engineering choices. Bonding alone does not prove breathability, waterproofness or wind resistance.
How does bonding affect seams?
A bonded fabric may be thicker, less compressible or less able to feed evenly than either layer on its own. The cut edge can expose several structures at once. A needle must pass through the complete stack, and the sewing operation can concentrate stress around holes and along the bond near the seam allowance.
For that reason, approve a sewn trial made with the production needle, thread, stitch, seam allowance, feeding setup and companion materials. Check:
- skipped stitches or needle damage;
- seam puckering and differential feeding;
- perforation or cracking near the stitch line;
- bulk at crossed seams and hems;
- local lifting of layers at cut edges;
- seam extension and recovery in the relevant direction;
- maximum seam force where a measured requirement applies.
ISO 13935-1 provides a strip method for maximum force to rupture a straight sewn seam, but its published scope is mainly woven fabrics and normally excludes coated fabrics. That limitation is important: a laboratory should confirm whether the method fits the exact bonded composite or select another agreed protocol. A generic seam test name is not evidence of a result.
What is delamination?
Delamination is separation between layers that were intended to remain joined. It can appear as edge lifting, bubbles, blisters, channels, local unbonded patches or a larger peel between components.
Not every visible line at a cut edge is delamination; separate layers can be visible while the bond remains intact. Conversely, a smooth face photograph can hide a weak bond. The meaningful question is whether the bonded structure remains within the agreed requirement after manufacturing, sewing, flexing, care and intended exposure.
Adhesive suppliers emphasize substrate compatibility and resistance appropriate to the end use. That matters because fiber and polymer chemistry, surface treatment, adhesive selection, activation, coverage, cure and later heat or washing can influence the bond. Without production records and testing, however, it is not responsible to assign a failure to one cause from appearance alone.
What should buyers test for delamination?
Start with an agreed control sample and a written protocol. ASTM D2724 is directly relevant to apparel: its current scope covers characterizing bond strength of bonded, fused and laminated apparel fabrics before or after laundering and drycleaning. The public ASTM page does not supply a universal pass number, so buyer and supplier must agree the requirement for the specific product.
A practical evaluation sequence is:
- Identify the stack. Record each layer, side, fiber or polymer description, construction, nominal mass, thickness and joining process.
- Map specimen direction. Mark machine/length and cross directions. Bond and stretch behaviour may differ by direction.
- Inspect the received sample. Photograph face, back, cut edge and any pre-existing bubbles, hard spots, strike-through or unbonded areas.
- Measure initial bond strength. Use the agreed laboratory method and report units, specimen width, direction, conditioning, peel geometry and failure mode.
- Apply the intended care exposure. ISO 6330 offers defined domestic washing and drying procedures. Select the actual relevant procedure; do not treat “machine wash” as a complete test condition.
- Recondition and re-inspect. Check the same locations for edge lift, bubbles, area separation, distortion, surface change and seam appearance. ISO 15487 can support appearance assessment after domestic care, but it is separate from bond-strength measurement.
- Repeat the bond measurement. Compare before/after results and note whether failure occurred within an adhesive interface, within a component or by another mode.
- Test the sewn construction. Examine seam allowances, curved areas, folds, hems and high-flex zones because a flat unsewn swatch does not represent every garment stress.
- Confirm the acceptance rule. State the minimum bond value, permitted visible separation, number of care cycles and sampling plan before bulk approval.
A quick hand peel can help screen samples, but it is not a controlled result. Hand force, angle, speed and specimen width vary too much. Use it to locate a concern, then use the agreed method for a decision.
What should be on a bonded-fabric specification?
At minimum, record:
- supplier and style code;
- intended end use;
- complete layer order from face to back;
- fiber content or material identity for each textile layer;
- adhesive, film, foam or joining process description where disclosure is available;
- nominal and tolerance values for total mass, usable width and thickness;
- face and back colour, texture and finish;
- stretch and recovery by direction;
- air, water-vapour, water-resistance or thermal requirements only when relevant;
- bond-strength method, direction, initial requirement and after-care requirement;
- washing, drying, drycleaning or other exposure sequence;
- seam construction and seam test where relevant;
- appearance limits for bubbles, strike-through, edge lifting and shade change;
- approved sample, lot identification and change-control rule.
This record prevents one common sourcing error: approving the visible face but leaving the backing, adhesive and test route undefined.
Where are bonded fabrics used?
Bonded composites can be engineered for apparel, footwear, bags, upholstery, automotive interiors, medical items, protective products and industrial materials. The breadth of these uses is another reason not to give the category one default performance profile.
Within apparel, possible constructions include face fabric joined to fleece, shell fabric joined to a film, or fashion fabric joined to an interlining. Suitability depends on the exact weight, hand, stretch, care, seam, safety and market requirements.
If your project is specifically a thermal or apparel program, the WellDoneTex Bonded Fabric page and Thermal Fabric Series provide commercial starting points. The separate thermal fleece buyer checklist covers product-specific sourcing questions for that narrower family. Those pages do not redefine the whole bonded-fabric category.
Final takeaway
Bonded fabrics are multilayer composites. They are made by joining at least two materials with an adhesive, heat-and-pressure process, ultrasonic points or another specified system. The face, joining layer and backing must be understood together.
Bonding can alter bulk, hand, drape, stretch, air pathways and sewing behaviour, but none of those outcomes is guaranteed by the category name. Verify the exact layer stack, process and performance claims on the real sample.
For delamination control, agree a measurable bond-strength requirement, test before and after the relevant care or exposure cycle, record failure mode, and inspect the sewn construction as well as the flat fabric. A clear specification is more useful than any generic promise that a bonded fabric is “strong,” “warm” or “waterproof.”
Related questions
Are bonded fabrics always laminated?
The terms often overlap, but usage varies. Both can describe multilayer composites. Ask for the actual layer stack and joining process instead of treating the words as a complete technical specification.
Is bonded fabric always waterproof?
No. Water resistance requires the right layers, construction, seams and verified test result. A fabric-to-fabric bond may contain no barrier layer at all.
Is bonded fabric always warmer than a single fabric?
No. A fleece or foam backing may add bulk and trapped air, while a thin film laminate may remain relatively light. Thermal behaviour belongs to the finished stack and test condition.
Can bonded fabric stretch?
Yes, some bonded fabrics stretch, but the finished composite may extend less than its most elastic component. Measure both directions on the complete material and report the method.
How can I identify bonded fabric?
Inspect both surfaces and a clean cut edge. You may see two textile structures, a film, foam or another backing. Visual inspection cannot identify adhesive chemistry or prove bond strength, so confirm with the technical record.
What causes delamination?
Several factors can contribute, including unsuitable substrate/adhesive compatibility, inconsistent application or cure, and exposure beyond the qualified care or use conditions. A failure analysis should examine production records, layer condition and measured failure mode rather than guessing from one photograph.
Is a hand-peel check enough?
No. It is useful only as a quick screen because force, speed, angle and specimen width are uncontrolled. Use an agreed laboratory method such as ASTM D2724 where its scope fits the product.
Does bonding change sewing requirements?
It can. Added thickness, compression, surface friction and limited stretch can change feeding and seam behaviour. Sew the real stack with production materials and inspect both the seam and nearby bond.
What should be tested after washing?
Recheck visible separation, bond strength, dimensional change, surface and seam appearance, stretch/recovery where relevant, and any product-specific performance claim. State the exact washing and drying procedure and number of cycles.
References
- PI Cottex. Bonded Fabrics: How Dual-Layer Construction Redefines Outerwear. Accessed 2026-09-12; product-specific performance claims excluded.
- ANDRITZ. Laminating. Accessed 2026-09-12.
- Bostik. Textile Lamination brochure. Accessed 2026-09-12.
- Covestro. Lamination. Accessed 2026-09-12.
- Coatema Coating Machinery. Textile. Accessed 2026-09-12.
- ASTM International. ASTM D2724-19(2025)e1 — Standard Test Method for Bond Strength of Bonded, Fused, and Laminated Apparel Fabrics. Accessed 2026-09-12.
- International Organization for Standardization. ISO 6330:2021 — Domestic Washing and Drying Procedures for Textile Testing. Accessed 2026-09-12.
- International Organization for Standardization. ISO 15487:2018 — Appearance of Apparel and Textile End Products After Domestic Washing and Drying. Accessed 2026-09-12.
- International Organization for Standardization. ISO 20932-1:2018 — Determination of the Elasticity of Fabrics — Part 1: Strip Tests. Accessed 2026-09-12.
- International Organization for Standardization. ISO 13935-1:2014 — Seam Tensile Properties — Part 1: Strip Method. Accessed 2026-09-12.
- U.S. Federal Trade Commission. Textile Fiber Rule. Accessed 2026-09-12.
- WellDoneTex. Bonded Fabric commercial product page. Read 2026-09-12.
- WellDoneTex. Thermal Fabric Series commercial category page. Read 2026-09-12.
- WellDoneTex. Thermal Fleece Fabric Buyer Checklist. Read 2026-09-12 as a narrower existing guide; its procurement modules are not duplicated here.